The MIP 4.0: connecting data, systems and operations for smarter pharmaceutical manufacturing
Industrial digitalisation goes far beyond incorporating new technologies. The real challenge lies in connecting processes, equipment and data to achieve more efficient, integrated operations and enable informed decision-making.
At Appliant, we continue to evolve our Manufacturing Intelligence Platform (MIP 4.0), a GMP-compliant solution designed to centralise plant and laboratory data, connect systems and optimise manufacturing processes within a single digital environment.
One platform. All your operations connected.
One of the main challenges in pharmaceutical manufacturing is the fragmentation of information across different systems, equipment and departments. This lack of integration can limit operational visibility, complicate data management and slow down decision-making.
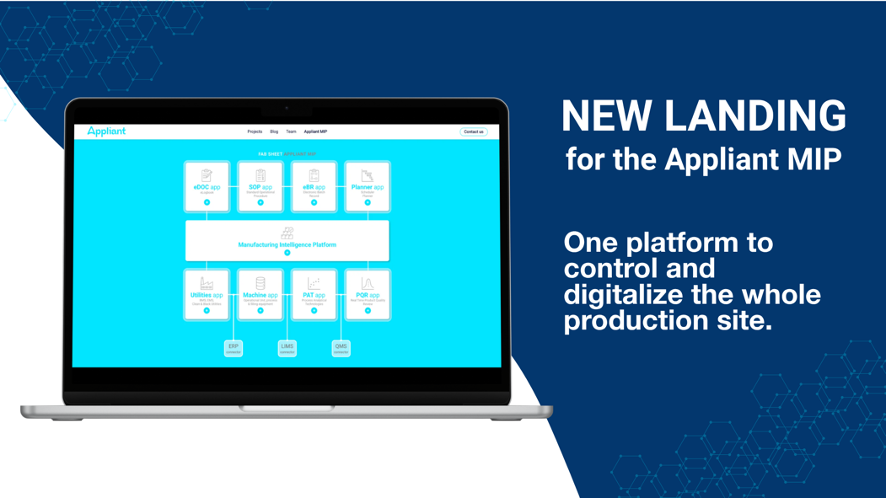
The MIP 4.0 addresses these challenges by bringing data and operations together in a single platform, providing comprehensive visibility from plant-wide operations down to individual equipment and sensors.
By connecting existing systems such as ERP, QMS and LIMS, the platform helps eliminate information silos and establish a Single Source of Truth (SST), ensuring that teams work with consistent, accessible and reliable information.
What's new in the MIP 4.0?
The latest evolution of the platform introduces an enhanced user experience and advanced functionalities designed to simplify daily operations and adapt to each organisation’s specific needs.
Key capabilities include:
- eBR with integrated lifecycle: digital management of electronic batch records, improving traceability, control and efficiency throughout production processes.
- Configurable workflows: flexible workflows adapted to each organisation’s procedures, helping standardise operations and streamline process management.
- Real-time monitoring: continuous visibility of processes, equipment and utilities, enabling faster access to operational data and more informed decision-making.
- Integrated data and systems: connectivity between different applications and existing industrial systems, reducing information silos and improving coordination across departments.
- Comprehensive operational visibility: centralised access to manufacturing information, from a global plant perspective to individual equipment and sensors.
Towards smarter, more connected pharmaceutical manufacturing
In highly regulated environments such as the pharmaceutical and biotechnology industries, reliable, accessible and traceable information is essential for maintaining operational control and supporting regulatory compliance.
With the MIP 4.0, Appliant helps manufacturers take the next step in their digital transformation, connecting people, processes and technology to improve efficiency, strengthen data integrity and support smarter manufacturing operations.
By bringing information together in a single digital environment, organisations can gain greater control over their processes and make better-informed decisions.
Discover what the MIP 4.0 can do for your plant
Ready to take the next step towards connected pharmaceutical manufacturing?
Book a demo with our team and discover how the MIP 4.0 can help you connect your systems, digitalise your processes and optimise your plant’s operations.
Featured in Partner Insights 2026
As an Ambit Iberia partner, we have participated for the second consecutive year in Partner Insights 2026, a publication that brings together partner companies and leading organizations within the Life Science ecosystem. This year’s edition highlights our role in developing GMP-validatable applications designed to digitalize and optimize manufacturing processes in the pharmaceutical and biotechnology industries.
Born from Klinea’s process expertise, Appliant integrates its solutions into the Manufacturing Intelligence Platform (MIP), using technology based on zenon and the Modular Type Package (MTP) standard. This enables modular, flexible, and scalable automation, with a validation package included.
This participation reinforces our commitment to the digitalization of manufacturing processes and to developing solutions that help organizations address today’s industry challenges, contributing to a more efficient, connected, and future-ready Life Science sector.